
—-|—————-|—————-|
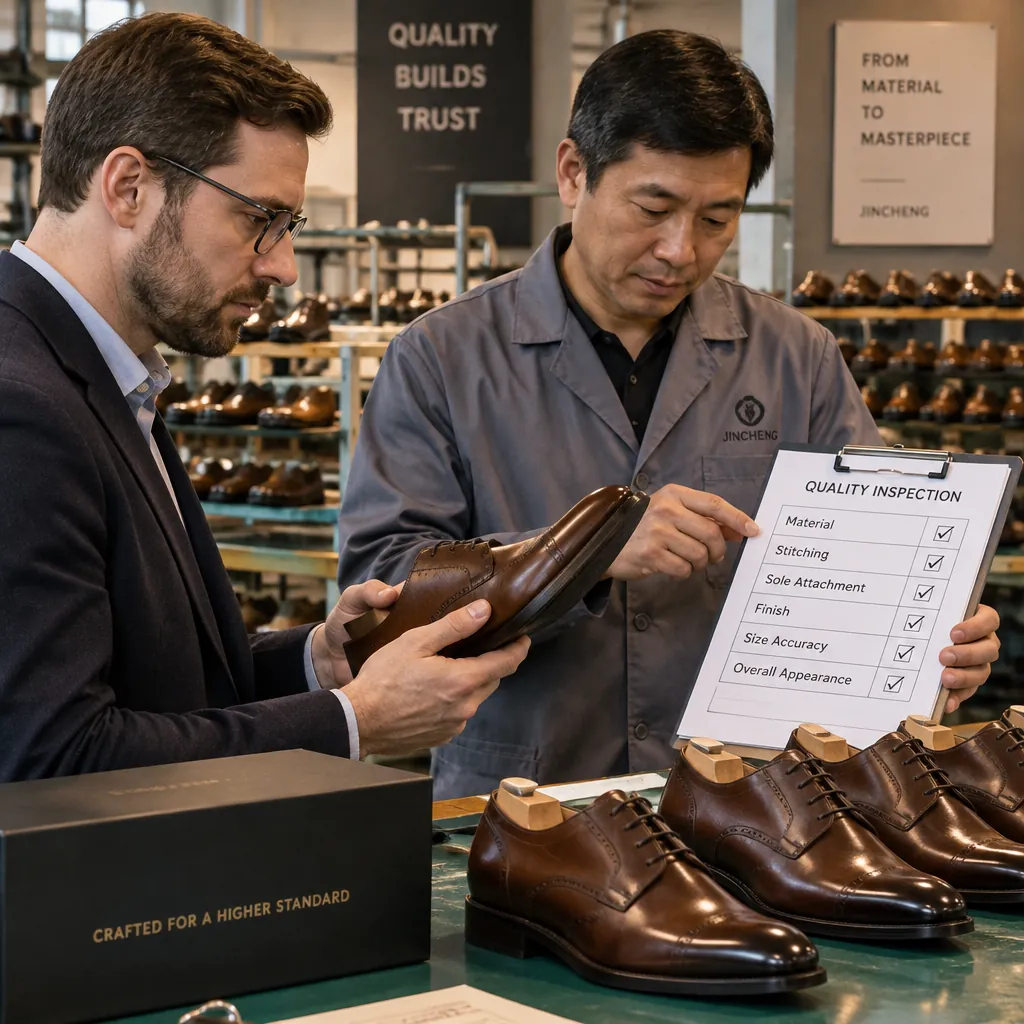
| Materials | Leather grade/thickness, lining, adhesives, hardware | Before cutting |
|---|---|---|
| Workmanship | Stitching, lasting, sole attachment, finishing | During production |
| Measurements & fit | Last confirmation, size grading, pair matching | First article + in-line |
| Compliance | REACH, CE/EN ISO 20347 scope, test reports | Before bulk + pre-shipment |
| Appearance & packing | Visual defects, pairing, labels, carton condition | Final random inspection |
One counterintuitive point experienced buyers internalize early: an inspection that “passes” does not mean zero defects. Sampling standards are built on probability — AQL 2.5 for major defects means a lot can still contain a small percentage of defectives and pass. What a pass does mean is that quality is inside the band you contracted for, which is why writing that band into the PO matters more than hoping the inspector catches everything.
Which Pre-Production Checks Prevent Problems Before They Start?
Pre-production inspection verifies that what the factory is about to cut matches what you approved. Three checks carry most of the weight:
Material verification. Confirm the upper leather matches the approved swatch on grade, thickness (measured at multiple points, not one), and finish. Check the lining, laces, eyelets, buckles, and outsole against the specification sheet. For adhesives and primers, ask for confirmation that formulations are free of restricted chemicals under REACH and your target market’s rules — a solvent issue found here is a paperwork problem, while the same issue found at customs is a shipment problem.
Pattern and last verification. The production last must match the fit-approved prototype, and pattern pieces must match the technical drawings, including seam allowances and grain direction. Size grading errors — where each size step drifts from the approved increment — are among the most expensive mistakes because they only surface when customers start returning sizes.
First article confirmation. Before the line runs at full speed, one complete pair from actual production materials should be pulled, measured, and compared against the golden sample. This is also the moment to confirm construction details matter to cost and repairability: a cemented sole and a Goodyear welt behave very differently when a pair comes back for repair, which we break down in our complete shoe construction comparison.
A note on what pre-production checks cannot do: they will not rescue a bad supplier choice. Verification assumes the factory wants to pass. Choosing a manufacturer with an established QC process — and a track record you can verify — remains the decision with the largest quality impact, which is why our manufacturer selection guide spends more pages on process evidence than on price lists.
What Should Be Verified During Production?
In-process (DUPRO) inspection catches systematic errors while they are still cheap to fix. For men’s dress footwear, the line checkpoints are:
- Stitching: consistent thread tension along the full seam, zero skipped stitches on visible lines, seam strength adequate for the stress point, no puckering on the vamp or quarter panels.
- Lasting: correct toe shape, centered backseam, no wrinkles in the lining under the heel, proper tack/heel-seat formation.
- Sole attachment: full and even bond line for cemented construction; consistent welt stitch for welted construction; no gaps at the shank area.
- Pair matching: matched grain, color, and finish between right and left shoes — a mismatch that is invisible on single shoes becomes obvious when a pair sits in a store display.
The most efficient in-process routine ties checks to the production stage: inspect upper stitching when the first 10–20% of uppers are done, check lasting output once the line warms up, and re-verify after any material changeover. If you cannot travel for mid-production checks, ask the factory for dated in-line photos tied to your PO number — a serious manufacturer keeps these as routine records, not as favors.
How Does Final Random Inspection Work Before Shipment?
Final random inspection (FRI, also called pre-shipment inspection or PSI) is the statistical gate before payment and loading. The standard reference is ISO 2859-1, the acceptance-sampling standard: you define a lot size, an inspection level (Level II is the default for most commercial orders), and acceptance quality limits — commonly AQL 2.5 for major defects and 4.0 for minor defects in footwear.
The mechanic in practice: for a 500-pair lot at Level II, the code letter points to a sample of 50 pairs. With AQL 2.5, acceptance is typically 3 defective pairs or fewer; 4 or more major-defect pairs fails the lot. The exact numbers shift with lot size, which is why buyers should fix the sampling plan in the purchase order rather than leaving “quality inspection” as a vague line item. Our dedicated guides explain how AQL sampling works for footwear quality control and which quality limits to set at each inspection stage.
Each sampled pair goes through a defined routine — a 3-second overall look, full checks of each shoe, pair matching, measurement sampling against the size chart, and packaging/labeling verification. Functional tests on dress shoes are lighter than on safety footwear but should still include heel attachment pull, bond integrity, and flex testing at the forefoot crease.
One honest boundary: third-party FRI protects you against process drift, but it does not replace contractual clarity. If the PO does not define defect classification (what counts as major vs. minor), the inspection report becomes a negotiation instead of a verdict. Write the defect examples down — crooked heel seats, loose threads on visible seams, color mismatch between pair halves, outsole bubbles, scorched lining edges — and both sides inspect against the same page.
Which Material Tests and Certificates Should You Actually Verify?
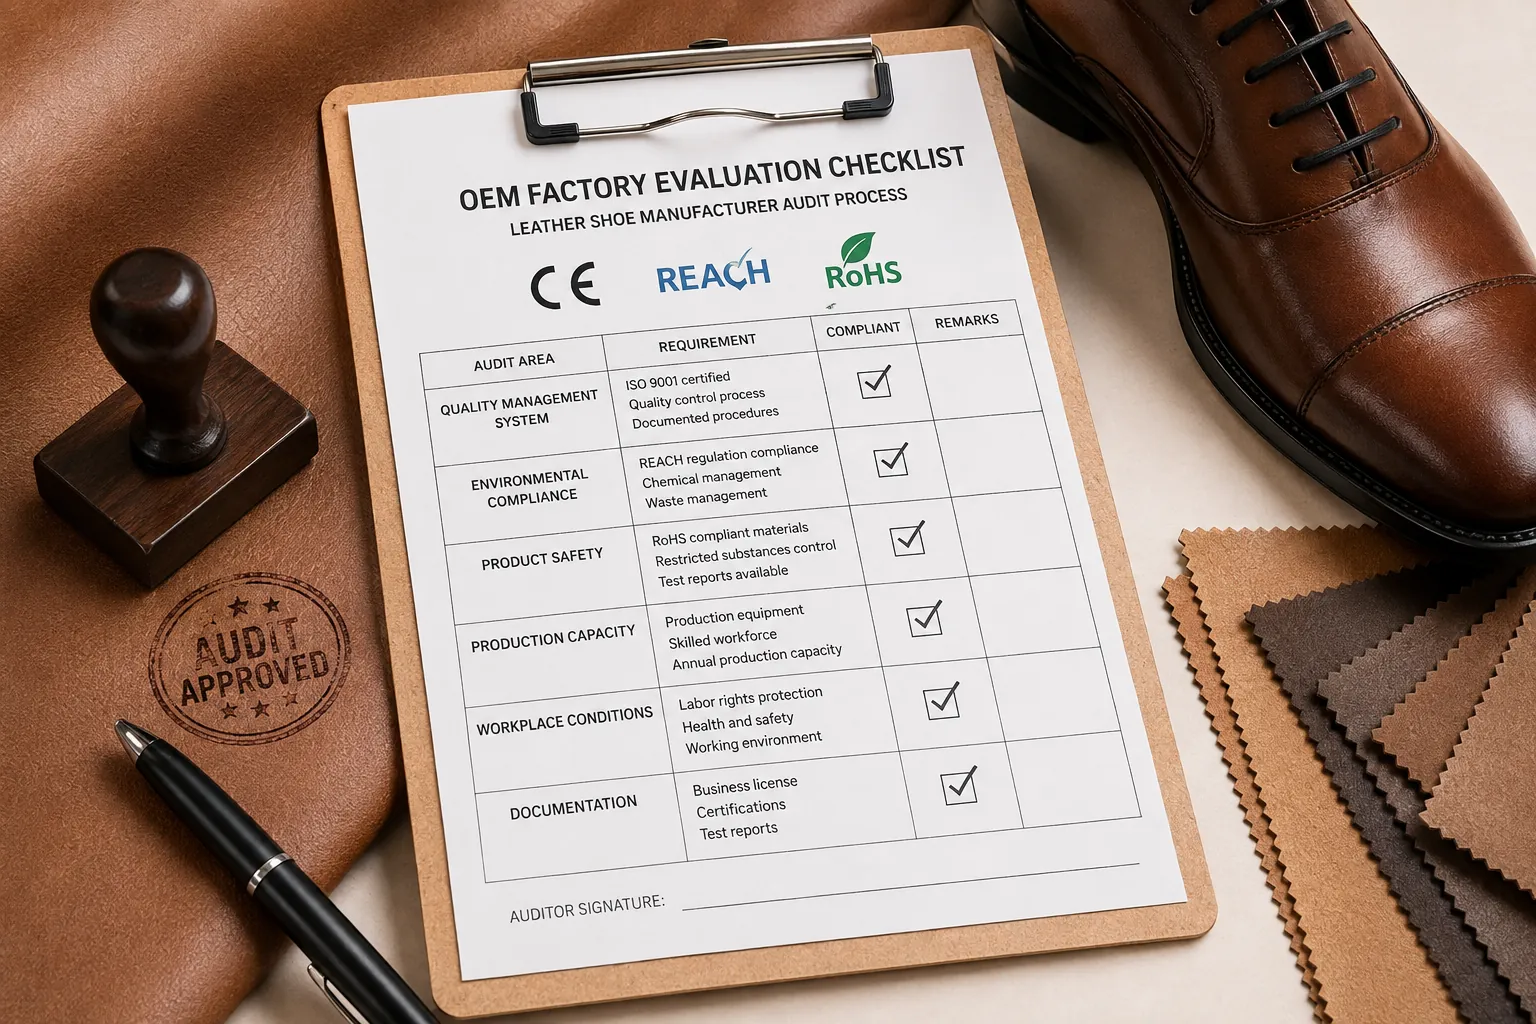
Chemical compliance is the part of shoe quality that never shows in a photo, which is exactly why it deserves document-level verification:
- REACH (EU): restrictions on azo dyes that can release carcinogenic aromatic amines, plus cadmium/lead limits and other substance restrictions. Ask for test reports from the actual production batch references, not just a certificate with no product linkage. The current list of substances restricted under REACH is maintained by ECHA and updated regularly — ask your supplier which version their reports reference.
- EN ISO 20347: this is the standard for occupational footwear (e.g., slip-resistant work shoes). General formal dress shoes for consumers are not automatically covered by it — if your use case is occupational, confirm the certificate scope covers the actual model, not just the factory in general.
- Physical tests: sole adhesion strength, flex resistance, heel attachment, colorfastness to rubbing. Accredited labs such as SATRA publish standard test methods for footwear, and report copies are a normal request in B2B transactions.
Verification practice that separates professionals from optimists: request primary-source documents, check that certificate scope names the product category and model family, confirm validity dates cover your delivery window, and match the report’s batch reference to your PO. A certificate that cannot be tied to your shipment is decoration.
Wincheer Shoes holds CE, REACH (Azo Dyes), RoHS, and EN ISO 20347 certifications covering its men’s leather footwear lines, so buyers can review certificate scope directly during sourcing. If CE marking is relevant to your program, our guide to CE-certified leather shoe factories in China covers what the marking does and does not guarantee.
What Should a Reusable Inspection Checklist Look Like?
The checklist below is written to be copied into your own PO documents. It compresses the four stages above into the items that decide most real-world disputes:
| Stage | Checkpoint | Pass criterion | Record |
|---|---|---|---|
| Pre-production | Upper/lining leather vs. approved swatch | Same grade, thickness in tolerance at 3+ points | Swatch photo + measurements |
| Pre-production | Hardware & laces vs. spec sheet | Function and finish match | Photo log |
| Pre-production | Last & pattern vs. fit-approved prototype | Identical dimensions and grading | First-article measurements |
| In-process | Stitching on visible seams | No skipped stitches; tension consistent | In-line photo (dated) |
| In-process | Sole attachment | Even bond/welt stitch, no gaps at shank | Sample pair kept |
| Final (FRI) | Sampling per ISO 2859-1, Level II | Per agreed AQL (typically 2.5/4.0) | Inspection report |
| Final | Measurements vs. size chart | Within stated tolerance | Measurement sheet |
| Final | Pair matching & packing | Matched grain/color; correct labels | Carton photos |
| Documents | REACH/EN ISO 20347 reports | Batch-referenced, in validity window | PDF copies on file |
Keep defect photos with the record — a classified defect library (what your inspector flagged, at which stage, with severity) is what turns a one-off inspection into a quality system. Over three or four orders, that library shortens every following negotiation because acceptance criteria stop being abstract. For the field habits that make this work, see our five practical footwear QC tips.
A last practical tip most first-time importers miss: pair this checklist with a small trial order instead of a full container. A 60-to-100-pair first order exercises the complete inspection loop — sampling plan, in-line records, FRI, corrective actions — at minimal risk. Our low-MOQ manufacturer guide explains how tiered pricing makes this workable.
How Should Buyers Respond When an Inspection Fails?
A failed final inspection is a process signal, not just a rejected carton. The professional sequence:
- Get the report classified: defect types, counts, and photos against the agreed AQL. Vague “quality issues” language is not actionable.
- Demand root cause, not just rework: a stitching failure fixed by re-stitching will recur unless the cause (needle, thread tension calibration, operator training) is identified.
- Agree corrective action with a date and re-inspect the reworked lot — at buyer’s choice of sampling level.
- Log it. A supplier’s failure history is the most honest input for your next sourcing decision.
Factories worth keeping will treat your failure report as useful data rather than an accusation. If a supplier resists documented corrective actions, that answer is itself information.
FAQ: Leather Shoe Quality Inspection for B2B Buyers
What AQL level should I use for men’s leather shoes?
Most footwear buyers apply AQL 2.5 for major defects and 4.0 for minor defects at General Inspection Level II. Premium lines sometimes tighten majors to 1.5; safety or occupational footwear (EN ISO 20347 scope) usually carries stricter plans. The right level depends on your market and price segment — decide it with your supplier before the PO, then hold it.
How many pairs get sampled in a final inspection?
Sampling size follows ISO 2859-1 tables: for a 500-pair lot at Level II, 50 pairs; for 1,200 pairs, 80 pairs. The counts are fixed by the standard, so insist your PO states lot size, level, and AQL together — that combination determines the sample size and accept/reject numbers.
Can I rely on factory self-inspection instead of third-party inspection?
Factory self-inspection with records (in-line photos, first-article measurements, internal FRI reports) is a legitimate baseline for established relationships. Third-party inspection adds value for first orders, new models, or after a failed lot. What self-inspection must never replace is the written acceptance standard — without agreed defect definitions, neither party can prove anything.
What are the most common defects in men’s dress footwear?
Recurring majors: asymmetric heel seats, open seams on visible stitch lines, color mismatch within a pair, outsole bond gaps, and toe shape deviation from the approved last. Recurring minors: loose threads, small finish marks, slight gloss variation. Your defect library will grow its own profile within two orders.
Does CE certification apply to formal leather dress shoes?
Not automatically. EN ISO 20347 covers occupational footwear — if you buy for hospitality, healthcare, or workwear programs, CE marking under that standard applies and the certificate must name the model. Consumer formal shoes are governed mainly by chemical rules such as REACH rather than a CE directive. Buy the certificate scope that matches your actual use case.
How long does sampling take before bulk production starts?
For men’s classic construction, plan 15–30 days for samples including revisions. Compressing this stage to save weeks usually costs more later — the fit-approved prototype and golden sample are the references your entire inspection chain depends on.
Get an Inspection-Ready First Order
If you are building a sourcing plan and want a factory that already operates the inspection loop described above — first-article records, in-line documentation, final random inspection against agreed AQL — send us your target styles. Wincheer Shoes Co., Ltd. has manufactured men’s leather footwear since 2007, producing oxfords, derbies, loafers, monk straps, and chelsea boots on production lines in Jiangmen, Guangdong (about 1.5 hours from Guangzhou), with warehouses and showrooms in both Shanghai and Jiangmen where buyer visits are welcome. First orders start from 60 pairs. Request a quote or sample plan through our contact page, or browse our oxford shoe and derby shoe wholesale collections to start the conversation with concrete references.
Sources / References: ISO 2859-1, *Sampling procedures for inspection by attributes* (via Acceptance sampling overview, retrieved 2026-09-18); REACH restrictions list, ECHA (via Wikipedia REACH overview, retrieved 2026-09-18); EN ISO 20347 *Personal protective equipment — Occupational footwear* (ISO/CEN, text reference); SATRA footwear test methods (satra.com, retrieved 2026-09-18).